Higher laser power can expand a fabrication shop’s processing options, but rated output alone says little about the number of acceptable parts produced during a shift. Actual results depend on material type, thickness distribution, cutting geometry, setup time, and how consistently the equipment operates between jobs.
Before investing in a 12 kW fiber laser cutting machine, manufacturers need to determine whether additional capacity addresses a measurable production constraint or simply raises the available ceiling. Hymson Laser Machinery operates in the industrial laser equipment sector, where evaluating practical performance against real manufacturing requirements provides a more useful basis for equipment decisions than relying on headline specifications.
Measure Throughput Beyond Cutting Speed
Machine throughput includes far more than the time the laser spends cutting material. Programming, loading, sheet alignment, part unloading, skeleton removal, and inspection can all affect how many finished components leave the production area. A faster cutting cycle may have limited impact if operators spend much of each shift handling materials or waiting for the next program. Production assessments should separate cutting time from non-cutting time to reveal which activities constrain overall output.
Part geometry also changes the relationship between speed and productivity. Long, uncomplicated contours may benefit substantially from higher cutting speeds, whereas intricate profiles with numerous small holes require frequent acceleration, deceleration, and direction changes. Piercing frequency and contour density can further affect cycle duration. Consequently, throughput estimates should come from representative parts rather than a single demonstration cut selected for its favorable geometry.
Batch structure matters just as much. Large runs of identical components allow programming and setup costs to be distributed across many parts, while frequent product changes introduce repeated preparation work. A workshop handling both production styles should evaluate output under each condition. The relevant measure is not simply the fastest possible cycle, but the number of saleable parts produced within the available operating hours.
Validate Cutting Quality Across Materials
Cutting quality needs to be evaluated across the materials and thicknesses that appear in normal orders. Edge roughness, dross formation, dimensional accuracy, heat effects, and perpendicularity may vary as material characteristics and process settings change. A successful test on one mild-steel sheet does not establish equivalent performance on stainless steel or aluminum. A structured trial should cover the material grades and thickness ranges that matter most to the workshop.
Process settings influence these outcomes in combination. Laser power interacts with cutting speed, focal position, assist-gas pressure, nozzle condition, and material surface characteristics. Raising power without adjusting other parameters may fail to improve the finished edge and can increase operating costs. Documenting settings alongside inspection results helps technical teams distinguish equipment limitations from process-development issues.
Quality validation should also include repeatability rather than a single acceptable sample. Multiple parts from different sheet positions or separate production runs can reveal inconsistencies that a brief demonstration misses. Dimensional measurements, visual edge checks, and downstream fit tests provide complementary evidence. For a high-power laser cutting machine, the important question is whether acceptable results can be reproduced under realistic production conditions, not whether one carefully prepared sample meets expectations.
Understand Acceleration and Machine Dynamics
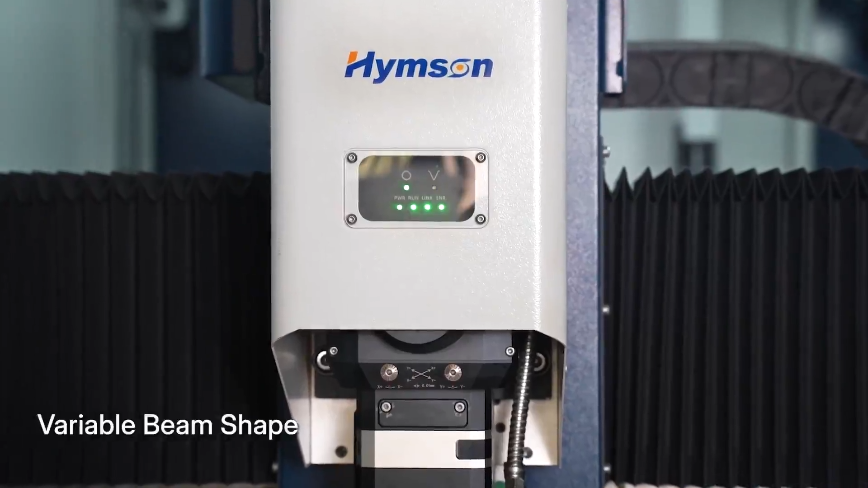
Cutting systems must manage frequent changes in direction and speed, especially when processing compact parts or dense nesting layouts. Acceleration affects how quickly the cutting head reaches the commanded speed after a turn, while mechanical rigidity and control behavior influence motion stability. On complex jobs, these characteristics may have a greater effect on cycle time than the maximum speed advertised for straight-line cutting.
The Hylaser PRO has a maximum X-Y-axis acceleration of 2.0 g, providing a specific reference for evaluating machine dynamics. That figure should be interpreted alongside positioning accuracy, contour performance, machine configuration, and test results; acceleration alone does not establish overall cutting productivity. Buyers should request demonstrations using representative parts so the interaction between motion behavior and actual cutting requirements can be observed.
Maintenance and operating conditions can also influence dynamic performance over time. Mechanical wear, alignment, lubrication, and the condition of motion components may affect repeatability if routine service is neglected. Evaluation should therefore consider maintenance intervals, inspection procedures, and the availability of technical support. Equipment performance is a continuing operational outcome, not merely a characteristic measured during acceptance testing.
Conclusion
Higher power is most valuable when it solves a clearly defined production problem, whether that involves recurring thick-material jobs, sustained throughput pressure, or a need for greater processing flexibility. Reliable decisions combine cycle-time measurements, repeatable quality checks, motion performance, utilization estimates, and realistic ownership costs.
The suitability of a high-power laser cutting machine depends on how its capabilities match the workshop’s production mix, while the value of a 12 kW fiber laser cutting machine should be demonstrated through measurable results rather than rated output alone. Hymson Laser Machinery can be assessed on the same basis: verified performance, documented operating requirements, and the practical fit between equipment and manufacturing demand.