A reliable pallet-conveyor supplier must translate load, route, takt, accumulation, positioning, safety, controls, and maintenance needs into a verifiable system design. The final pallet transport specification is stronger when it records this point: Drawings, samples, and acceptance criteria reduce the chance that commercial language will be interpreted differently after ordering.
A supplier of pallet conveyor must prove load handling, routing, positioning, controls, safety, maintenance access, commissioning, and support. Fair comparison of pallet transport alternatives depends on a common premise: A representative trial reveals interface problems that a catalogue comparison may not expose.
Realistic testing of pallet transport has to reproduce this situation: Quality evidence matters most when it can be traced to the same configuration and production conditions proposed for the order. Interfaces around pallet transport work better when teams recognize this dependency: Feeding trials should use the real component range because geometry, surface condition, orientation, refill behavior, and jams interact.
Translate the Application into Conveyor Data
Quality control for pallet transport improves after this variable is defined: Factory and site acceptance should use agreed products, recipes, staffing, utilities, and pass windows so results represent production conditions. Delivery of pallet transport becomes more predictable with this scope clarified: Service responsibilities need named owners, response expectations, spare-parts logic, and a method for controlling later changes.
Pallet-transport specifications should define automated pallet conveyor systems against measurable loads, interfaces, operating assumptions, and acceptance evidence. Maintenance planning for pallet transport benefits from the following design choice: A controlled sample is a starting point for validation, not automatic proof that every future batch will behave identically.
Pallet-transport selection should consider the supplier’s engineering, fabrication, verification, commissioning, and long-term maintenance capabilities together. Expansion of pallet transport remains practical when this provision is retained: The final decision should record unresolved assumptions so they can become contract conditions or commissioning checks.
Documentation for pallet transport becomes useful when it captures this evidence: Cross-functional review keeps engineering, procurement, quality, and operations aligned around one version of the requirement. Commissioning of pallet transport succeeds more often when this behavior is tested: Supplier assessment should connect engineering ownership, manufacturing capacity, verification records, delivery resources, and lifecycle support.
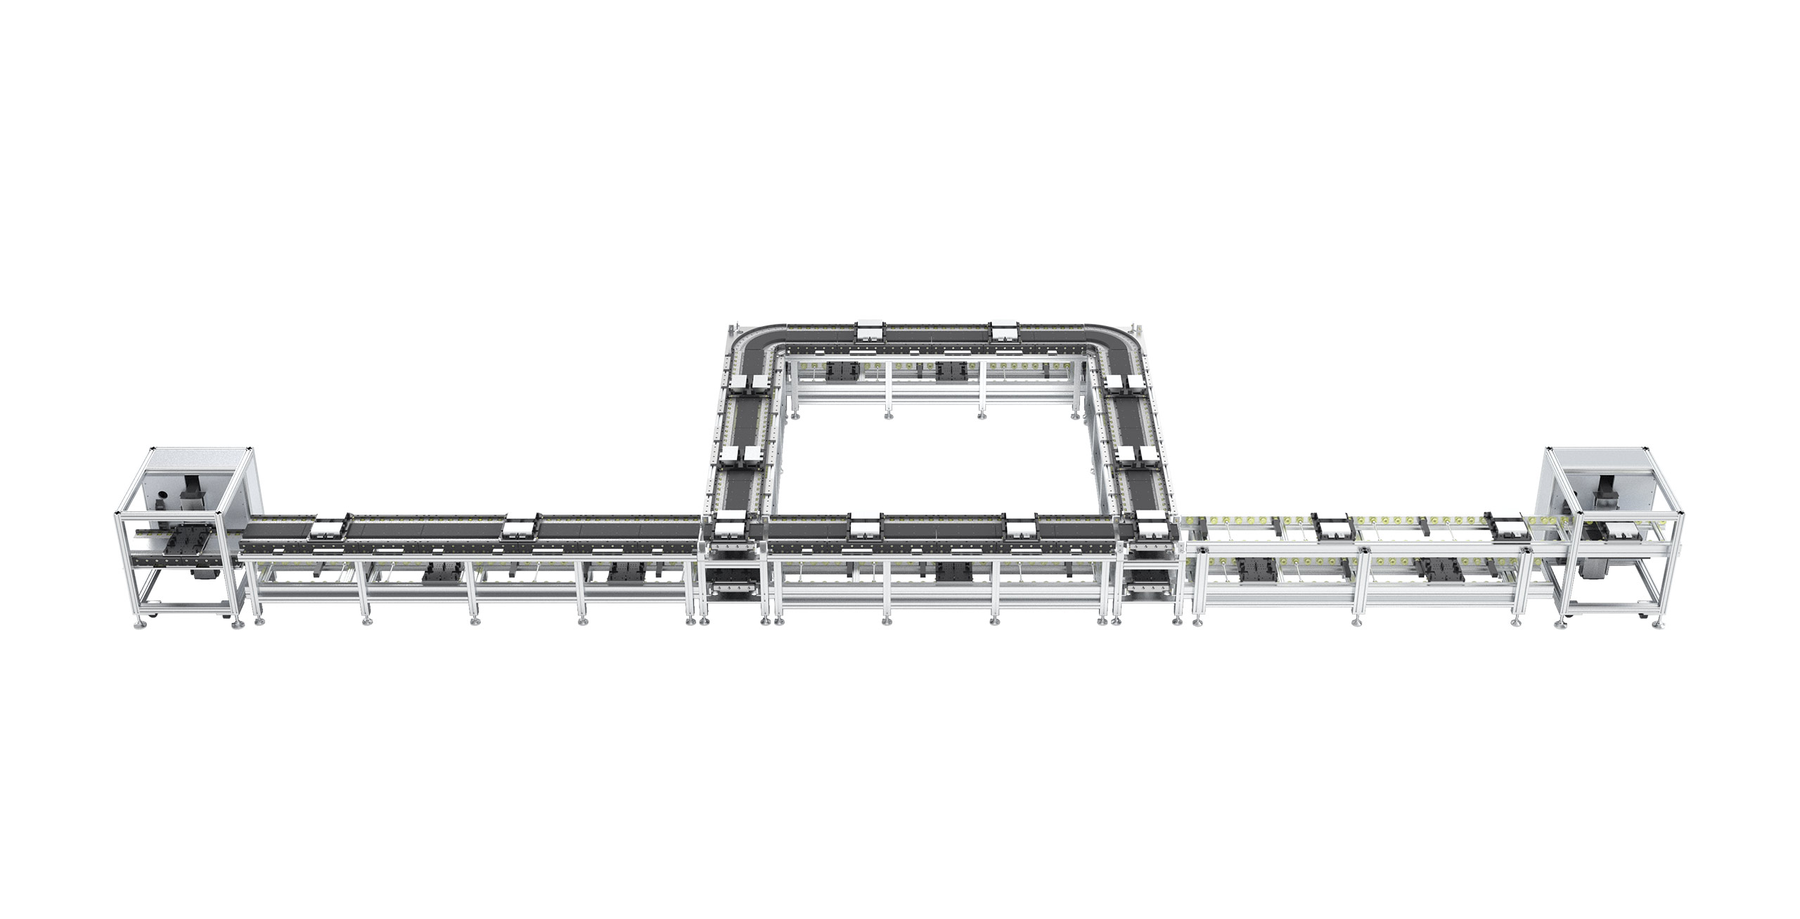
The manufacturer’s automated pallet-transfer system has ±0.1 mm repetitive positioning accuracy, a 5–40 kg load range, maximum thrust of 100 N, and maximum speed of 2.5 m/s. Recovery from a pallet transport fault is faster when this capability exists: Measurements are more persuasive than adjectives because they allow two alternatives to be assessed on the same basis.
Suppliers of pallet transport can be compared fairly against this requirement: Control, motion, sensing, processing, inspection, software, and transport must exchange dependable states before the line can behave as one system. Standard aluminum profiles make it easier to mount sensors, brackets, and accessories, while modular molded components simplify maintenance and support medium-load transport.
Assess Mechanical and Control Capabilities
The published range includes pallet widths from 160 to 1,200 mm, line lengths from 600 to 12,000 mm, and speed up to 20 m/min for the double-plus conveyor family. Clear pallet transport specifications avoid ambiguity by recording this detail: Product-specific tooling and recipes should be separated from the common platform when variants or later models are expected.
Production using pallet transport remains stable when this condition is controlled: Measurement capability must be established before inspection results are used for rejection, compensation, or process-control decisions. Service planning for pallet transport improves when this responsibility is explicit: Routing logic should define priority, blocking, buffering, mover identification, station readiness, and recovery after a transport fault.
Controls associated with pallet transport earn confidence through this result: PLC, motion, sensing, robotics, process equipment, inspection, and transport must exchange reliable states and fault information. Investment decisions on pallet transport sharpen when this factor is quantified: Flexible transport creates value only when routing rules cover priority, blocking, station readiness, buffering, and recovery from a transfer fault.
Operating limits for pallet transport become clearer beside this evidence: Automotive programs gain resilience from modular tooling and controlled interfaces that can accommodate model changes without rebuilding every station. Handover of pallet transport is complete only when this item is documented: MES records become useful when product identity follows process parameters.
Pallet Transport comparisons retain automated pallet conveyor systems beside the agreed configuration, workload, interfaces, test method, and release criteria. Batch consistency for pallet transport improves when this reference is retained: Feeding trials should use the real component range because geometry, surface condition, orientation, refill behavior, and jams interact.
Choose a Supplier for Lifecycle Reliability
Field performance of pallet transport remains credible under this condition: MES data is valuable when it supports a production or quality decision rather than merely increasing the number of stored tags. Purchasing decisions about pallet transport hold up when this fact is verified: Delivery planning needs design freeze, long-lead procurement, assembly, software integration, testing, shipment, installation, and ramp-up.
Technical review of pallet transport progresses once this boundary is known: A useful specification separates mandatory limits from preferences that can be traded against price or lead time. Validation of pallet transport becomes repeatable when this method is fixed: Long-lead equipment, software integration, customer approvals, shipment, site utilities, installation, and ramp-up belong in one delivery schedule.
Pallet-transport release documentation should keep pallet conveyor linked to the approved dimensions, configuration, verification results, and batch-control requirements. The commercial scope of pallet transport is clearer after this issue is resolved: Maintainability depends on access, diagnostics, spare strategy, training, recovery procedures, and clear ownership when the line stops.
Material choices for pallet transport are grounded in one practical point: The accepted solution then needs configuration records, test evidence, change control, training, spare-parts logic, and recovery ownership. A conveyor supplier becomes a dependable lifecycle partner by proving load handling, routing, positioning, controls, safety, maintainability, commissioning, and support against the customer’s line.
Responsibility for the pallet transport handover is clearer when FHS and the buyer preserve the approved configuration, acceptance results, change history, and support ownership. A realistic pallet transport brief gives particular weight to this fact: Supplier assessment should connect engineering ownership, manufacturing capacity, verification records, delivery resources, and lifecycle support.